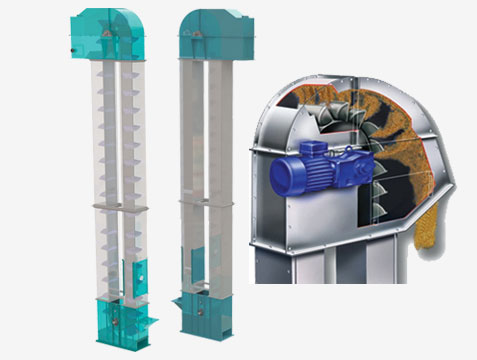
Bucket elevators are used to convey granular products vertically. Thanks to their efficiency and small footprint, they are preferred for conveying granular bulk materials up to 50 mm in size.
Features and Advantages
High efficiency with low power consumption
Easy and minimal maintenance
Easy access points for cleaning
Durability and long service life
Trouble-free operation
Small installation area
Technical Specifications
The elevator top head is manufactured as a removable steel structure. If required, the top head can be dismantled in two sections.
Connections are designed with bolts.
Elevator pipes are manufactured from press-formed sheet metal.
Elevator pipe sections are manufactured with a maximum length of 3 metres.
One of the pipe sections is removable to allow the buckets to be fitted.
Specially designed flanges are formed on the pulley to prevent the belt from deviating from the pulley.
Covers are provided on the upper and lower heads for easy cleaning and maintenance.
Dust extraction openings are provided on the lower and upper elevator sections to allow dust to be extracted from inside the elevator.
A glass inspection cover is positioned at a suitable viewing distance so that elevator operation can be observed.
A durable black rubber belt or a white nylon-reinforced belt is used in the elevator.
Sheet-metal, stainless-steel and plastic buckets can be used in the conveying system.
The drive drum is manufactured from cast material.
The gearbox is connected to the drive drum by a star coupling.
A belt tensioning system is provided on the lower elevator.
Drum shafts are secured by bearing housings.
Motor: Specifications vary according to elevator capacity, the product to be conveyed and the elevator height.

 Turkish